
A cheese producer required a complete end-of-line automation solution capable of handling cheese blocks from incoming wooden racks through inspection, case packing, palletizing, and final pallet wrapping.
The objective was to reduce manual product handling, improve process consistency, maintain food-industry hygiene standards, and provide better visibility into production performance.
The Challange
Cheese blocks arrive at the end-of-line area stacked on wooden shelf racks. Each block must be removed from the rack, transported through the line, labelled, weighed, inspected, and prepared for shipment.
Depending on the production order, the cheese blocks may be:
- packed into individual cartons before palletizing; or
- transferred directly to the palletizing station without secondary packaging.
The system therefore had to support different production routes while maintaining reliable product flow and minimizing manual intervention.
The customer also required automatic handling of wooden racks, quality-control integration, production-data reporting, and a complete pallet-finishing process.
PERUZA Solution
From standartized solutions PERUZA developed a complete food-grade end-of-line system that takes cheese blocks from the depalletizing area to a wrapped and labelled pallet ready for shipment.
PERUZA Robot Depalletizer
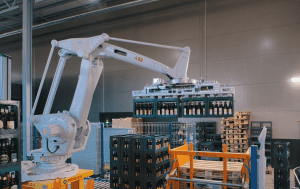
A six-axis robot equipped with a custom-designed PERUZA pneumatic gripper removes wooden shelf layers containing cheese blocks from the incoming pallet.
PERUZA Robot Depalletizer places the products onto the conveyor system, creating a controlled and continuous flow toward the inspection and packing stations.

Product Labelling and Weighing
Each cheese block is automatically labelled according to its size and production requirements.
The system supports:
- top and bottom print-and-apply labelling for larger cheese blocks;
- top and bottom labelling for smaller cheese blocks; and
- label sizes of up to 100 × 150 mm.
Every cheese block passes through an integrated metal detector and checkweigher.
Products that do not meet the specified weight or inspection requirements are automatically removed from the main production flow and transferred to a dedicated reject and accumulation area.
This allows quality-control procedures to be completed without stopping the entire line.

PERUZA Top Load case packer
PERUZA Top Loader is a case packer which packs products directly from above.
Pre-cut carton blanks are automatically positioned, folded, and sealed using hot glue. The cheese block is therefore fully packed without requiring operators to manually form cartons or handle the product during the packing process.
When cartons are not required, the control system can route unpackaged cheese blocks directly toward the palletizing station.

PERUZA Robot Palletizer
PERUZA Robot Palletizer palletizes products according to the selected pallet pattern.
The robot can also place slip sheets between pallet layers when required. Product recipes stored in the control system allow operators to select the appropriate pallet configuration for each production order.
After palletizing, the completed pallet passes through an automated finishing sequence that can include:
- pallet positioning;
- 90-degree pallet rotation;
- print-and-apply pallet labelling; and
- automatic stretch wrapping.
The finished pallet leaves the line labelled, secured, and ready for storage or shipment.

Wooden Rack Washing Integration
The wooden shelf racks used to transport and accumulate cheese blocks must also be cleaned before returning to production.
To support this process, PERUZA developed an automated rack-washing system that can be integrated into the same end-of-line area.
Dirty racks are transported by conveyor into a rotating-brush washing unit. After washing, they are transferred to a clean conveyor and collected by the depalletizing robot.
When required, the robot can be supplied with a higher-payload configuration and additional gripper tooling, allowing it to handle the racks and rotate them upside down during the operating cycle.
Together, these systems show how PERUZA approaches end of line solutions with standartized products.
Preparing Food and Beverage Production for Future Growth
As production volumes continue to increase and labour becomes more difficult to source, investing in automation is becoming a strategic necessity.
Automated secondary case packaging, improves efficiency, reduces operating costs and helps manufacturers maintain consistent packaging quality across different product formats.
Whether packaging cheese, dairy products, beverages, or other food products, the right case packer can streamline end-of-line operations while creating a scalable packaging process ready for future growth.
Choosing the right case packer depends on your product, your speed requirements, and how your line is laid out- every production floor is different.
Our team can walk through your specific needs and recommend the right equipment for your line. Contact PERUZA Sales engineer Hugo Grube at hugo.grube@peruza.com to explore the right case packing and see already made solutions for your business.